
Plywood manufacturing · Ha Hoa, Vietnam
Plywood manufacturing process: how plywood is made in 14 steps
In short
The plywood manufacturing process at Minh Thanh Plywood runs in 14 steps, from plantation logs around Ha Hoa, Vietnam, to a sealed container. Logs are peeled into veneer, dried, sorted, glued and cross-laid into stitched cores, pressed twice, calibrated, faced, sanded, caliper-checked, packed and filmed at loading. We produce 50,000+ m³ a year.
Watch the film
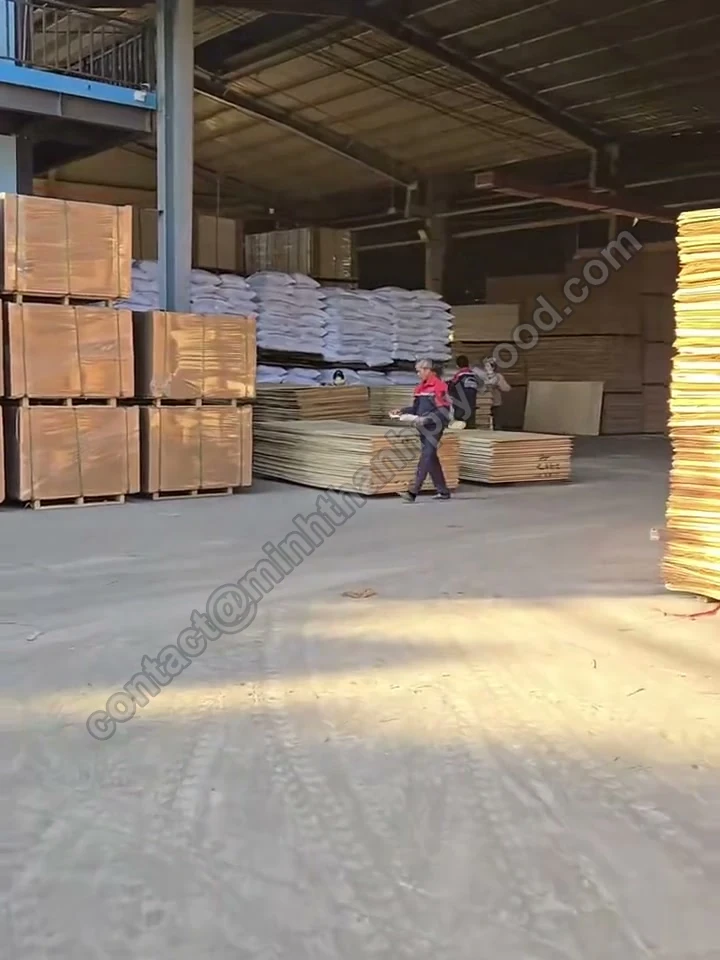
Watch plywood being made: 14 steps on the factory floor
The film shows the plywood manufacturing process at Minh Thanh Plywood in 2 minutes 40 seconds: real footage of each of the 14 steps from plantation log to sealed container, with the key number of every step on screen. Watch it first, then read each number in full on this page.
Chapter 1, core making (steps 1–3): plantation logs peeled into core veneer, veneer drying on racks, then jointing on the core composer and stitching of the outer core layers.
Chapter 2, two-press panel making (steps 4–9): glue spreading, cross-laid lay-up, the cold pre-press and the hot press, calibrating sanding, hand repair of the core, then face veneer and a second press.
Chapter 3, finishing and dispatch (steps 10–14): finish sanding, trimming and cut-to-size, caliper checks, export packing and the filmed container loading, closing on the proof documents and what to send for a quotation.
Proof
Plywood production you can verify.
Every step on this page runs under an audited quality system and a chamber-tested glue line. These are the English originals; full copies go to buyers by email.
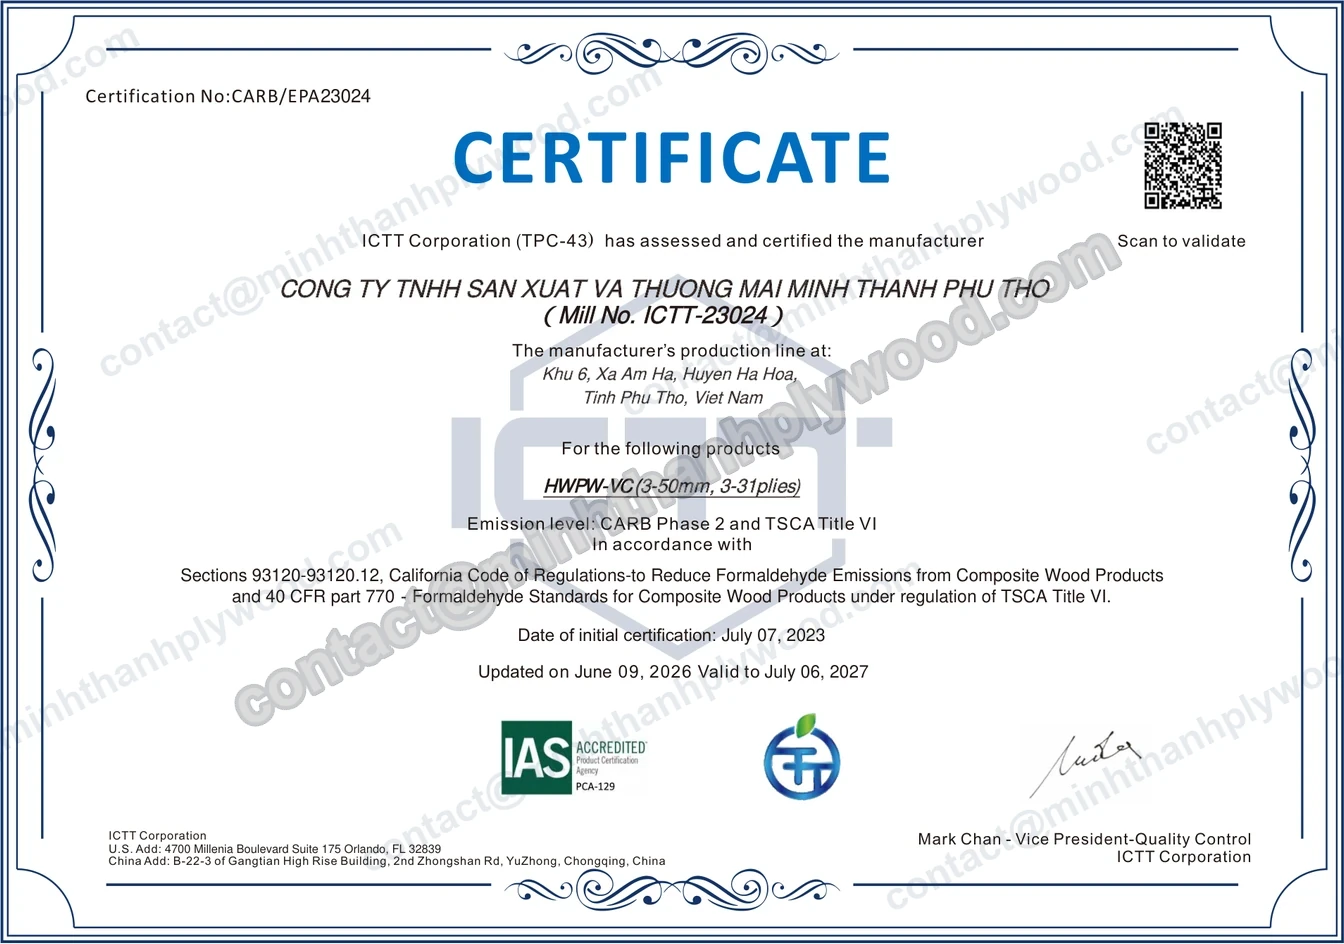 CARB P2 / TSCA Title VIICTT mill no. 23024 · hardwood plywood, 3–50 mm
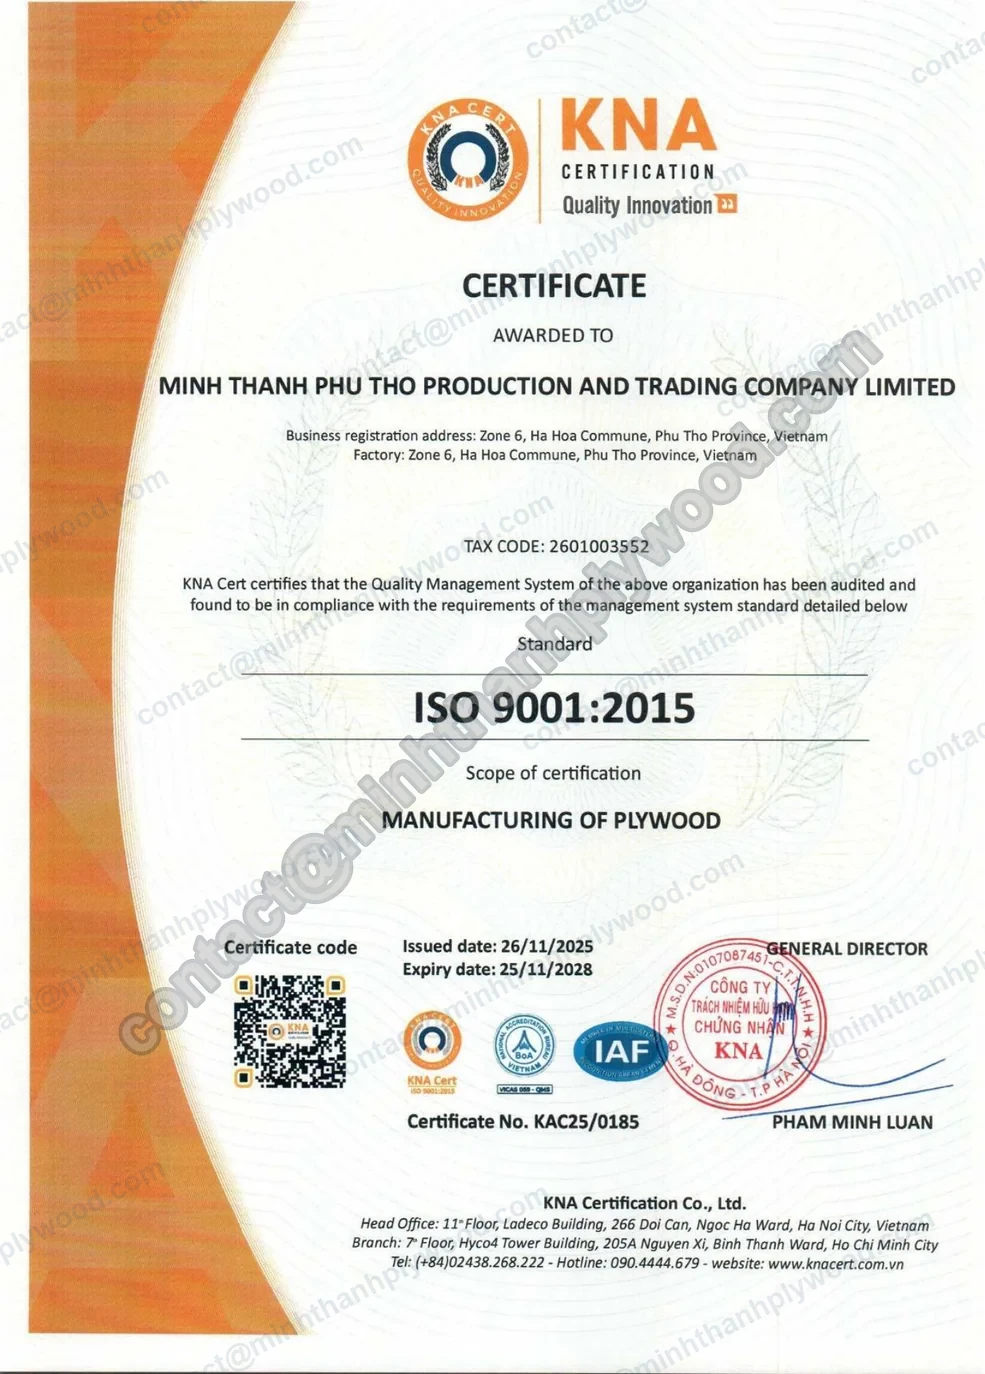 ISO 9001:2015Quality management system for plywood manufacturing · KAC25/0185
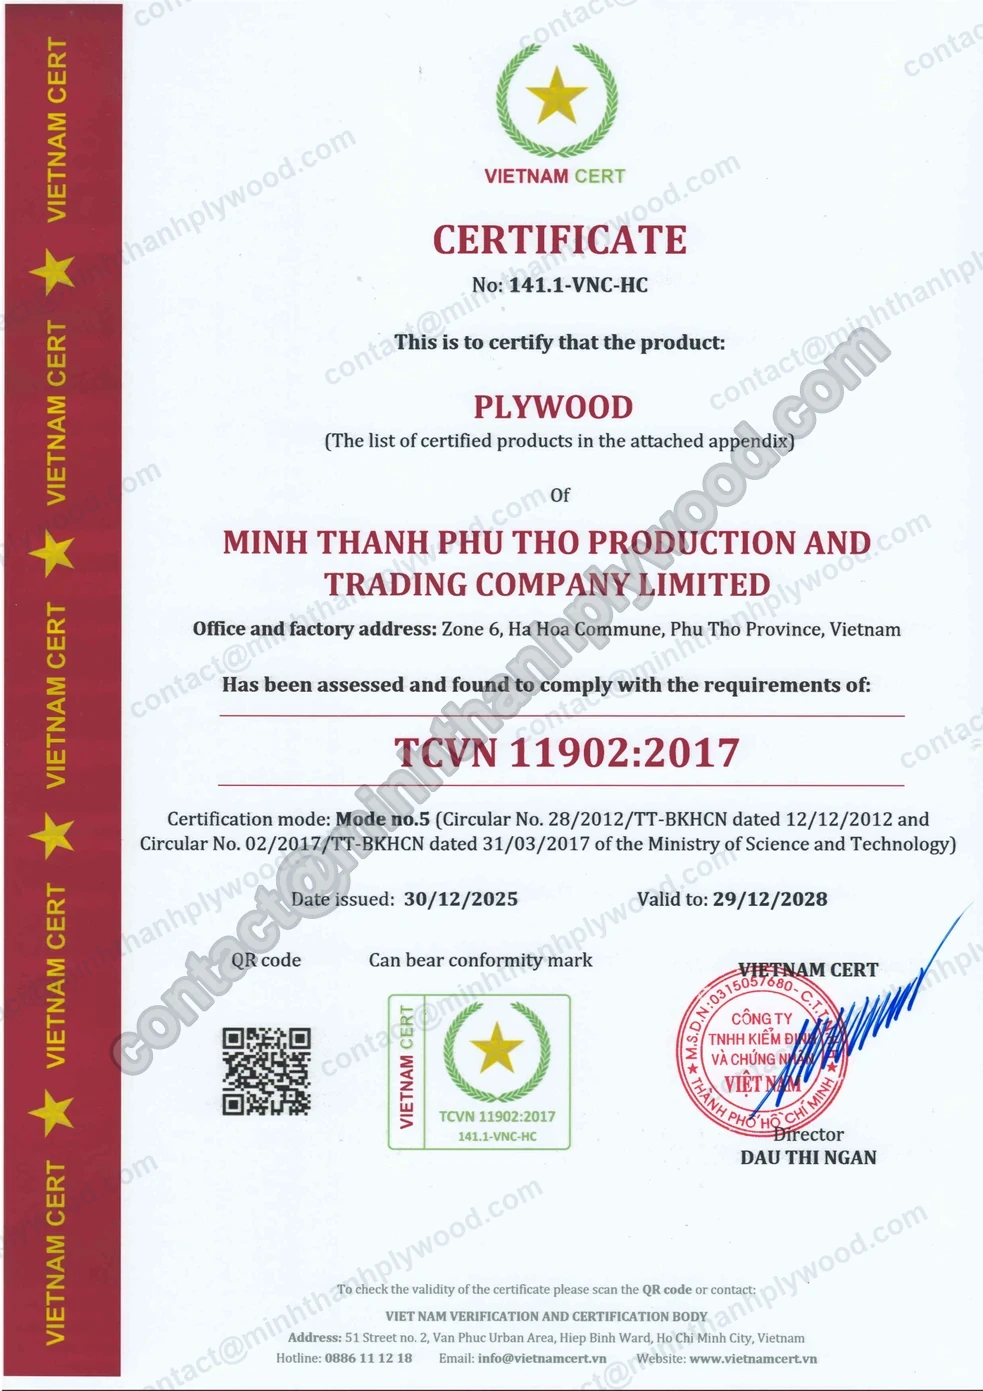 TCVN 11902:2017Vietnam national standard for veneer-faced plywood
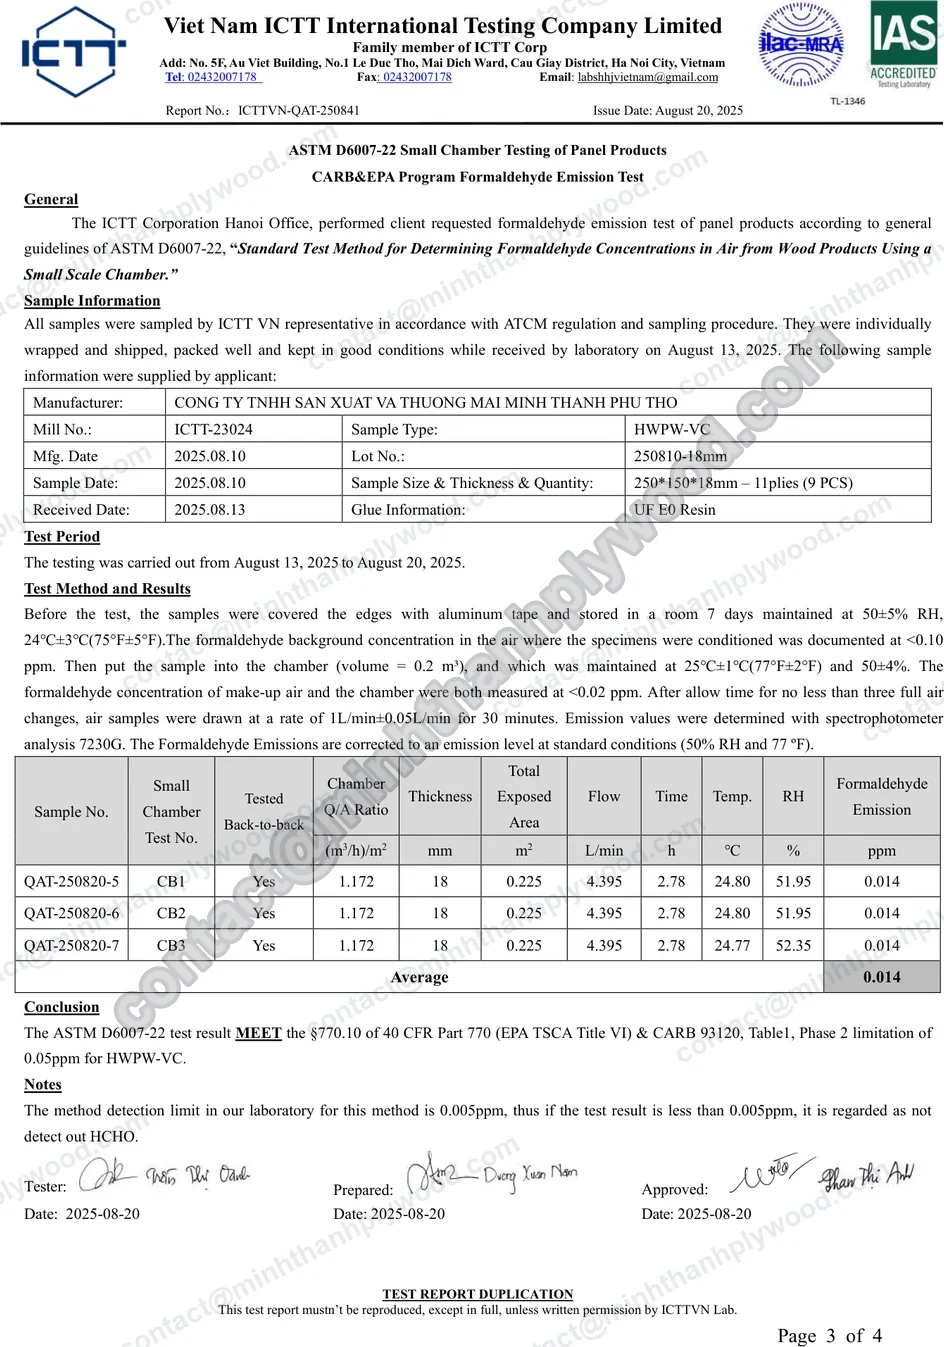 E0 emission testASTM D6007 chamber, Shanghai Hongjun and ICTT Vietnam · six tests 0.014–0.032 ppm vs 0.05 ppm limit · repeated every 3 months
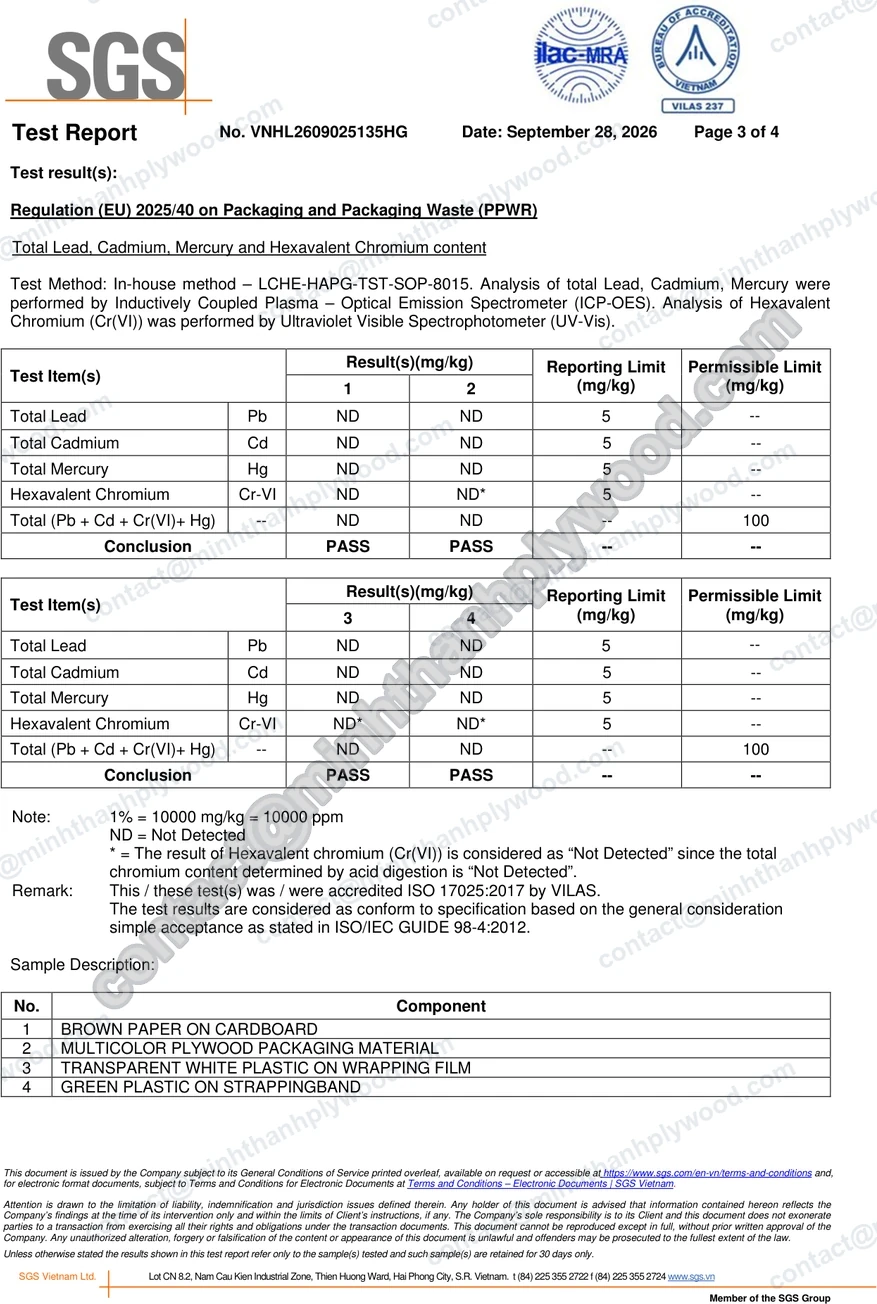 PPWR packaging testSGS, September 2026 · heavy metals not detected
How is plywood made?
The plywood manufacturing process at a glance.
Plywood is made in 14 steps grouped in three phases: core making, two-press panel making, then finishing and dispatch. The table lists every step with what happens and its key number.
In shortPlywood is made by peeling logs into thin veneer, drying it, spreading glue on it and laying the sheets with the grain of each layer at 90° to the next. Heat and pressure bond the stack into one panel, which is then sanded, trimmed, inspected and packed. An odd number of cross-laid plies keeps the panel flat and stable.
| Step | Machine | What happens | Key number | Check |
|---|---|---|---|---|
| 01 Logs and peeling | Debarker, rotary lathe | Plantation logs are debarked and rotary-peeled into core veneer | Core veneer 1.4–2.0 mm | Log size, splits |
| 02 Drying and sorting | Open drying racks, sorting table | Veneer is dried, then sorted; splits, holes and soft wood come out | 8–12% moisture | 8–12% moisture, splits out |
| 03 Jointing and stitching | Core composer, stitching machine | Narrow pieces are jointed into full sheets; outer core layers stitched | Outer 2–4 layers, both ways | No open joints |
| 04 Glue spreading | Roller glue spreader | Glue is rolled onto the core veneers to the order | UF glue at E0 standard; MR or WBP glue, E1, to order | Glue type and class as ordered |
| 05 Lay-up | Lay-up station | Veneers are cross-laid at 90° into a balanced, odd-ply stack | 18 mm: 11–13 plies | Ply count, 90° cross |
| 06 Cold pre-press | Cold press | The glued stack is pressed cold to flatten it and fix the layers | 3–5 kg/cm², 10–20 min | Stack square |
| 07 Hot press | Multi-opening hot press | Heat and pressure cure the glue and bond the core | MR 110–120 °C, WBP 130–145 °C; 8–12 kg/cm² | Bond on samples |
| 08 Calibrating sanding | Calibrating sander | The pressed core is sanded to an even thickness on both sides | Thickness set before facing | Even core thickness |
| 09 Repair and face lamination | Hand repair, hot press | Defects are filled, face and back veneers glued on, pressed again | Face veneer 0.2–0.5 mm | Face against sample |
| 10 Finish sanding | Wide-belt sanders | Faces are sanded and polished smooth | Both faces UV-ready | Sanding marks |
| 11 Trimming and cut-to-size | Trim saws | Panels are trimmed square to size or cut into smaller pieces | 1220×2440 or 1250×2500 mm | Size ±2 mm |
| 12 Quality control | Digital caliper, boil tank | Thickness, faces, edges, bond and count checked against the order | Caliper on every pack | Caliper every pack, boil test |
| 13 Export packing | Packing line, steel strapper | Packs are counted, covered, cornered and strapped on pallets | 18 mm ≈ 55 sheets a pack | Sheet count, labels |
| 14 Container loading | Forklift, camera | Packs are loaded, photographed and filmed before sealing | Up to 18 packs per 40HC | Photos, video, seal |
Press temperature follows the glue system and thickness tolerance follows the product line; the numbers table gives each value with its condition.
What plywood is made of
Raw materials: cores, faces and glue.
Plywood is made mostly of wood veneer and glue. What changes from one mill to the next is the species, the veneer grade, the glue type and the emission class. These come first in every specification.
| Material | Source | Thickness | Character | Used for |
|---|---|---|---|---|
| Styrax core (white core) | Plantations in northern Vietnam, around Ha Hoa | 1.4–2.0 mm core veneer; 1.3 mm in 4 mm panels | Cream-white, light: panels about 500 kg/m³ | Furniture and interior plywood, thin plywood, more m³ per container |
| Eucalyptus core | Plantations around Ha Hoa | 1.4–2.0 mm | Pinkish-brown, harder: panels about 650 kg/m³ (650–750) | Furniture panels that need weight and screw holding, commercial plywood |
| Acacia core | Vietnamese plantations | 1.4–2.0 mm | Medium weight: panels about 580 kg/m³ | Commercial, packing and film-faced plywood |
| Face and back veneers | EV, poplar, birch, okoume, pine; also bintangor, eucalyptus, gurjan, sapele on request | 0.2–0.5 mm; 0.3 mm common for Europe | Graded by your approved sample | The visible faces; the product is named after the face |
| Glue type (sets the bond) | Mixed to the order | Spread on the core veneers | Urea-formaldehyde (UF) for interior; melamine-fortified (MR) for humid use, about 12 h boil; phenolic (WBP) for exterior | UF for furniture and interiors; MR or WBP for damp and outdoor use |
| Emission class (sets formaldehyde) | Set by the resin recipe, tested in a chamber | Applies to the whole panel | E0 standard (0.014–0.032 ppm in ASTM D6007 tests); E1 to order | E0 for furniture, interiors and the US, EU and Japan markets |
| Film overlay | Phenolic film, to the order | 120–135 g/m²; premium from 135; anti-slip about 220 | Brown or black, sealed edges | Film-faced and anti-slip plywood |
Glue type and emission class are two separate lines in a specification: the glue type sets bond strength and water resistance, the emission class sets formaldehyde release. Vietnamese plywood cores are Styrax, eucalyptus, acacia or mixed; there is no poplar or birch core: birch-faced plywood is birch veneer on a Vietnamese core.
Plywood manufacturing process, step by step
How plywood is made: 14 steps from log to container.
These are the steps for our furniture and interior panels, each with a photo from the line, what happens, its numbers and the check that closes it. Commercial, packing and film-faced lines skip or simplify some steps.
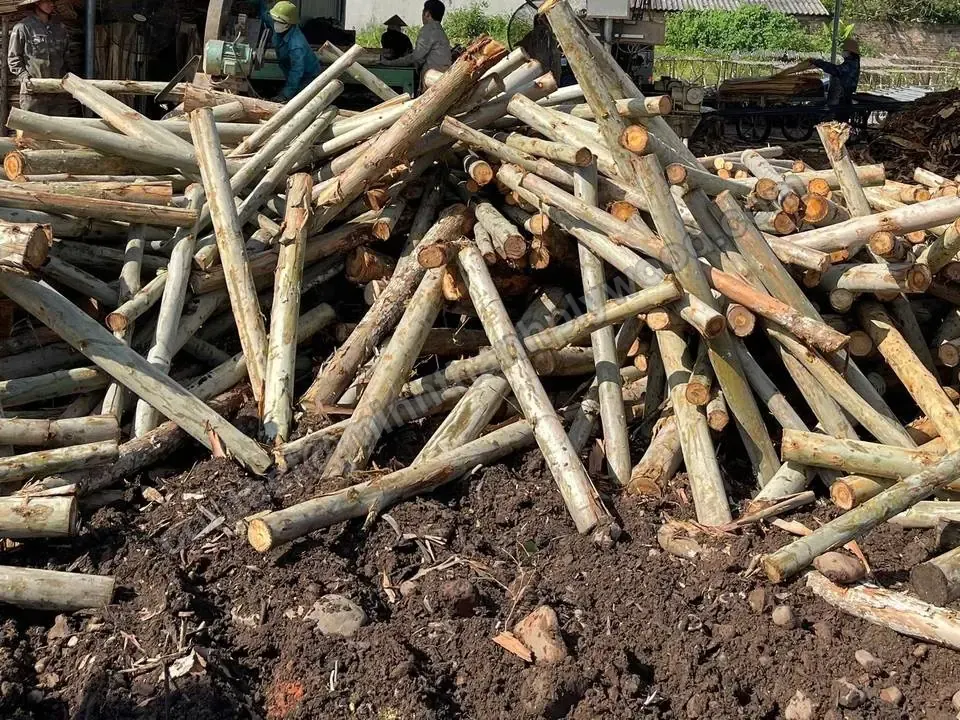
Debarked plantation logs waiting at the peeling line. 01Plantation logs and rotary peeling
Core timber comes from eucalyptus and Styrax plantations around Ha Hoa in Phu Tho province. Fresh logs are debarked and turned on a rotary lathe, which peels one continuous ribbon of veneer from the log. Plantation logs reach the lathe within a short haul, so they peel green and smooth without long soaking.
- Styrax and eucalyptus from local plantations
- Core veneer peeled about 1.4–2.0 mm thick
- 1.3 mm core veneer for 4 mm panels
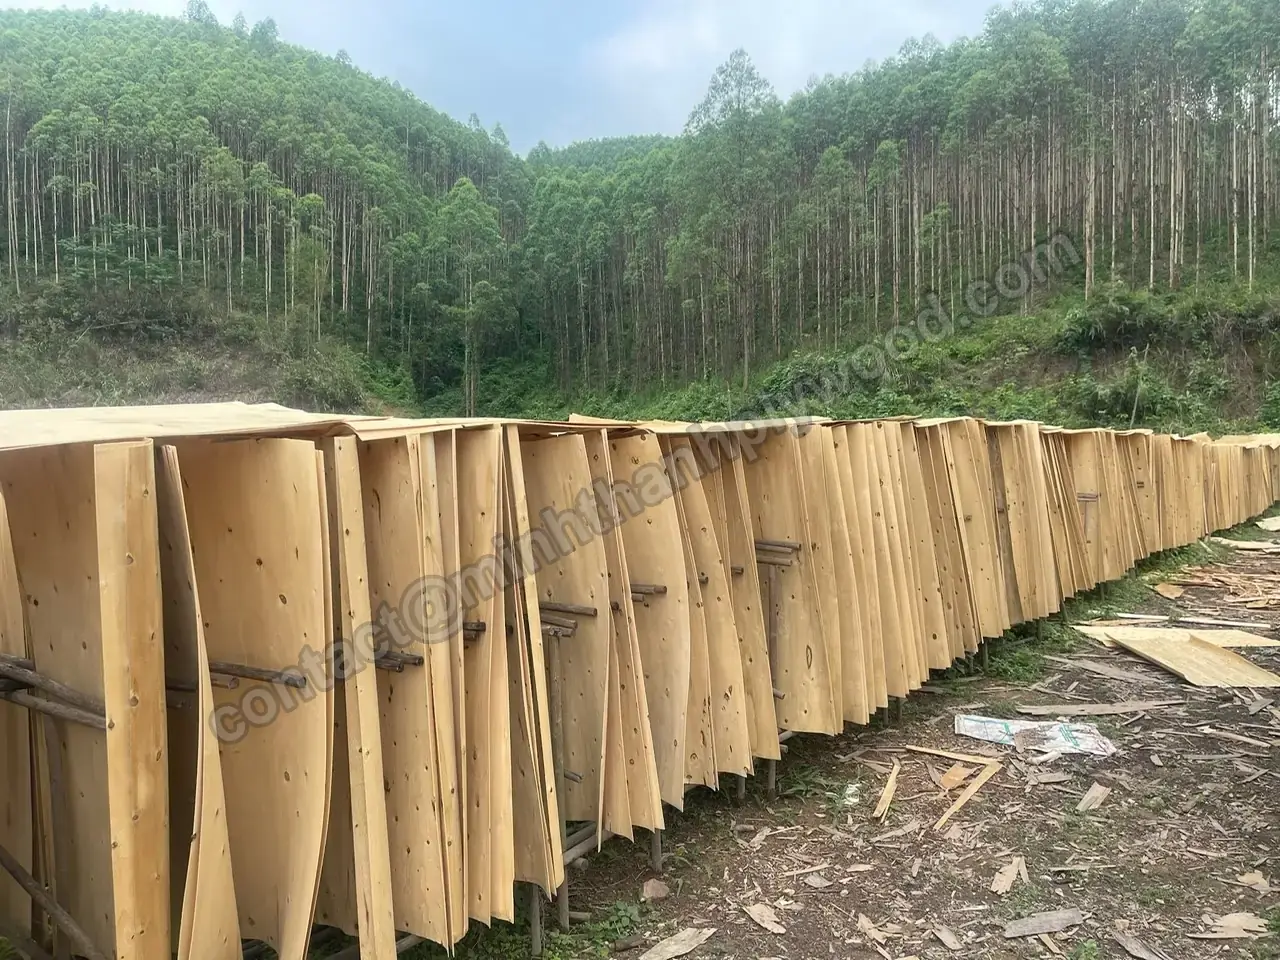
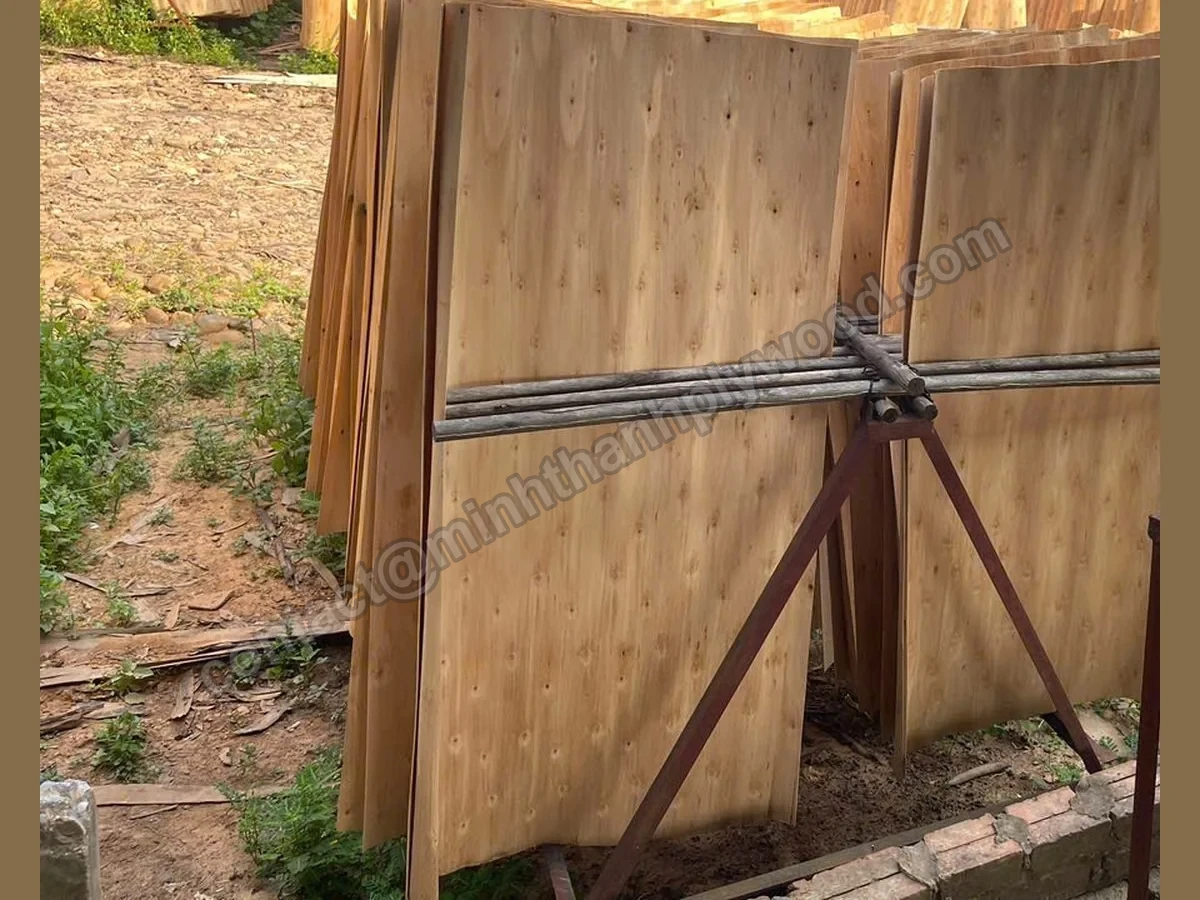
Core veneer drying on racks, plantation hills behind. 02Drying and sorting the veneer
Fresh veneer is wet, so it is dried before it meets glue. Core veneer is sun-dried on open racks in the plantation air; drying continues until the moisture suits the glue, 8–12%. Dry sheets are then sorted: splits, holes, soft wood and off-size pieces are taken out.
- Moisture brought down to 8–12% before gluing
- Splits, holes and soft wood sorted out
- Face veneer graded against your approved sample
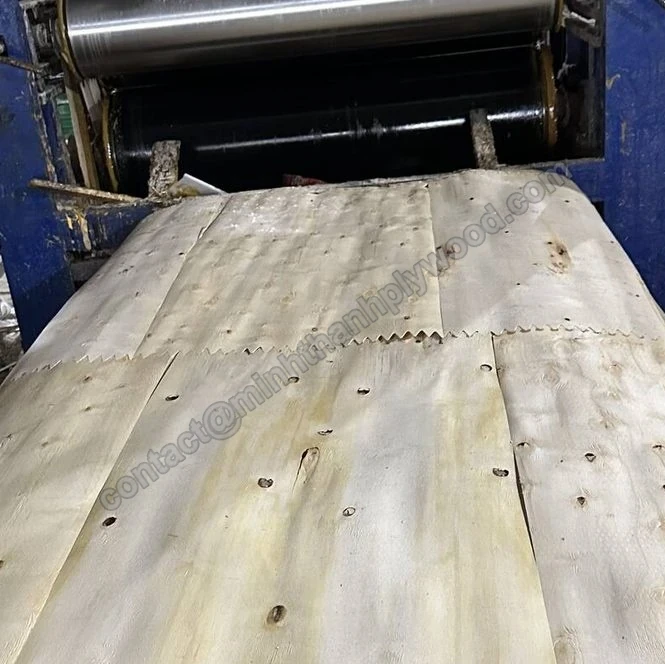
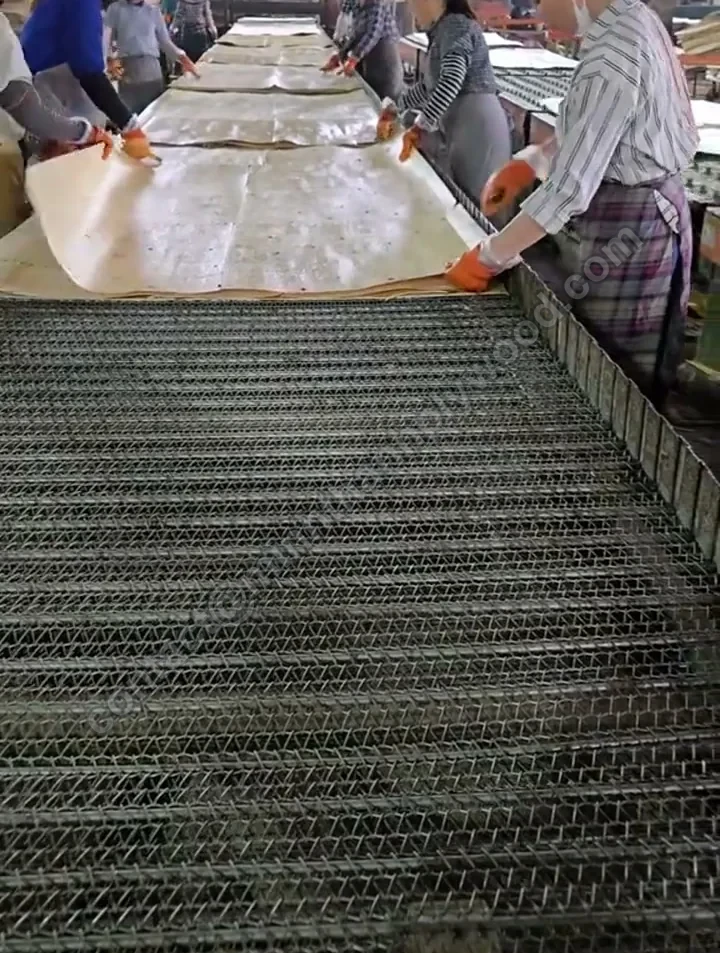
Core veneer pieces jointed into one sheet on the composer. 03Core jointing and stitching
Narrow strips of core veneer are jointed edge to edge on a core composer into full-size sheets. For furniture panels the outer 2–4 core layers are also stitched horizontally and vertically, so joints cannot open in the press. Stitching all layers is available on request.
- No open joints or overlaps in a core sheet
- Outer 2–4 core layers stitched both ways
- All layers stitched on request
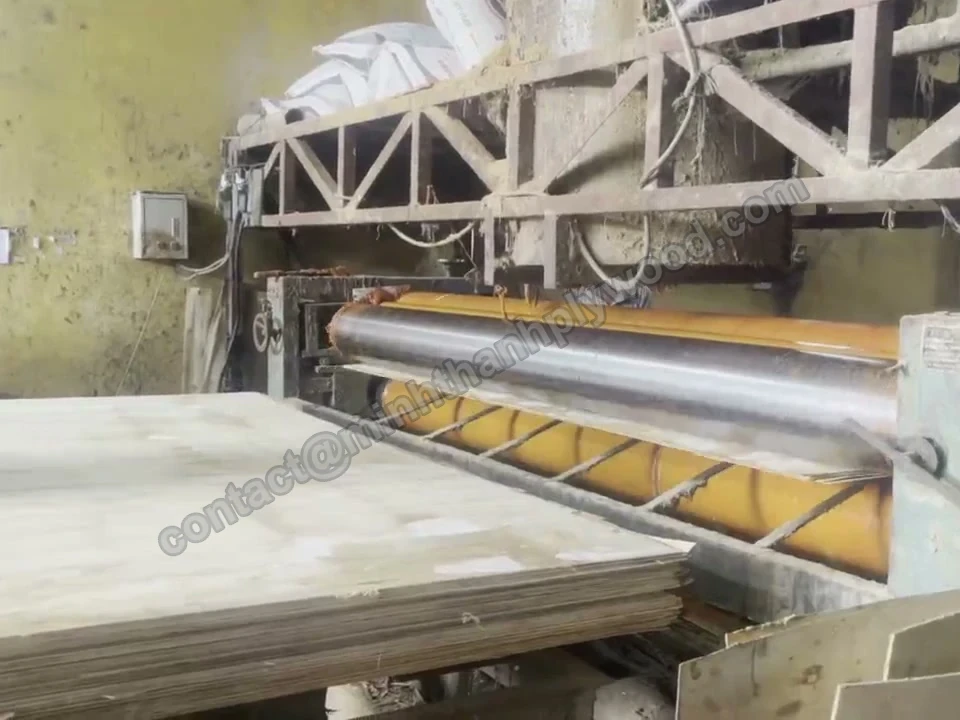
Roller glue spreader with core sheets ready to coat. 04Glue spreading
Core veneers pass through a roller glue spreader that coats both sides evenly. Two choices are mixed to your order. The glue type sets the bond: UF for furniture and interiors, MR or WBP when the end use needs more water resistance. The emission class sets formaldehyde: E0 as standard, E1 to order.
- Glue type and emission class as ordered
- Even spread on both sides of the core veneer
- Glue line tested later by boil test (step 12)
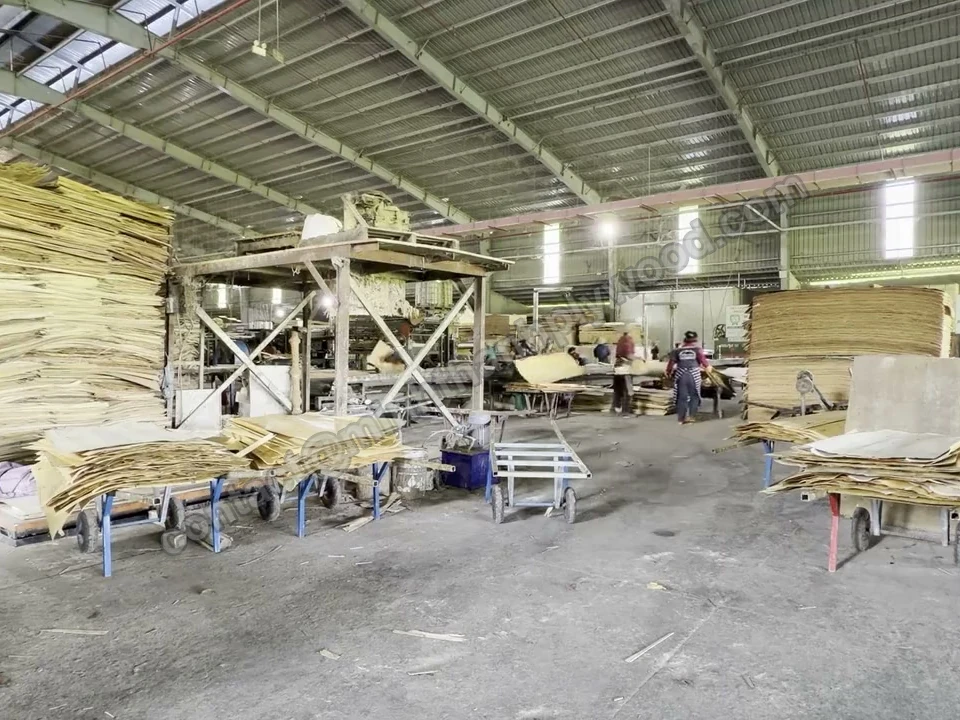
Lay-up stations with core veneer stacked ready to build. 05Lay-up: cross-laying the plies
Glued and dry veneers are laid one on another with the grain of each layer at 90° to the next. The stack is always an odd, balanced number of plies so the panel stays flat. An 18 mm panel is 11–13 plies, most often 11; thin 3–5 mm panels are always 5-ply.
- Grain crossed at 90° layer by layer
- Ply count matched to thickness
- Gaps and overlaps fixed before pressing
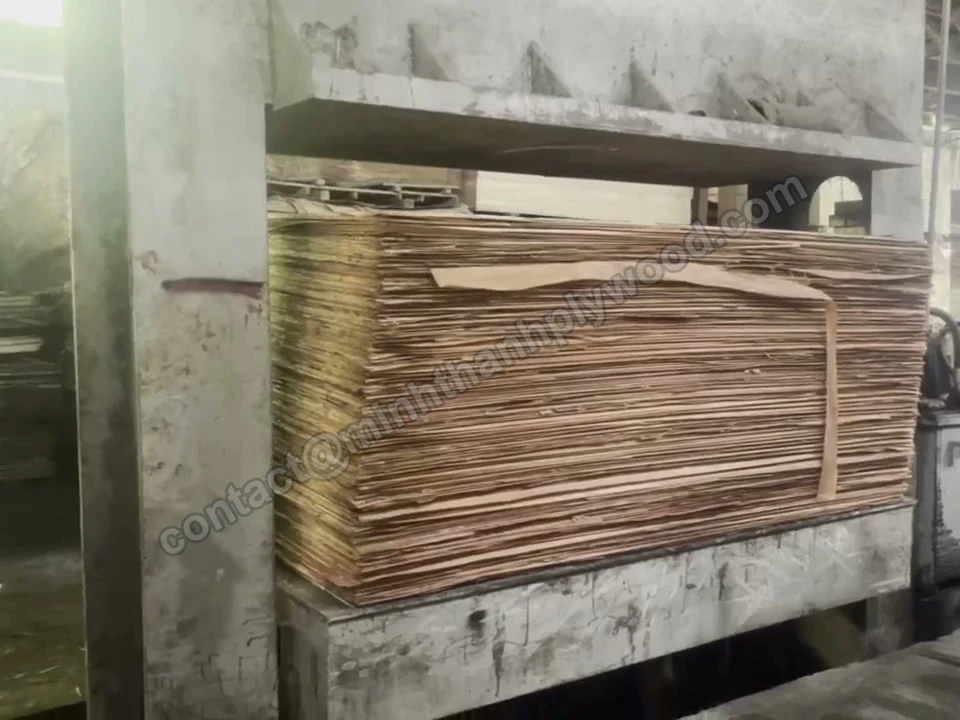
Glued cores in the cold pre-press. 06Cold pre-press
The laid-up stack goes into a cold press first, at a moderate 3–5 kg/cm² for 10–20 min. Pre-pressing flattens the veneers, lets the glue tack and fixes the layers, so each panel enters the hot press square and without shifted plies.
- 3–5 kg/cm² for 10–20 min
- Layers fixed so they cannot shift in the hot press
- Loose or shifted plies corrected here
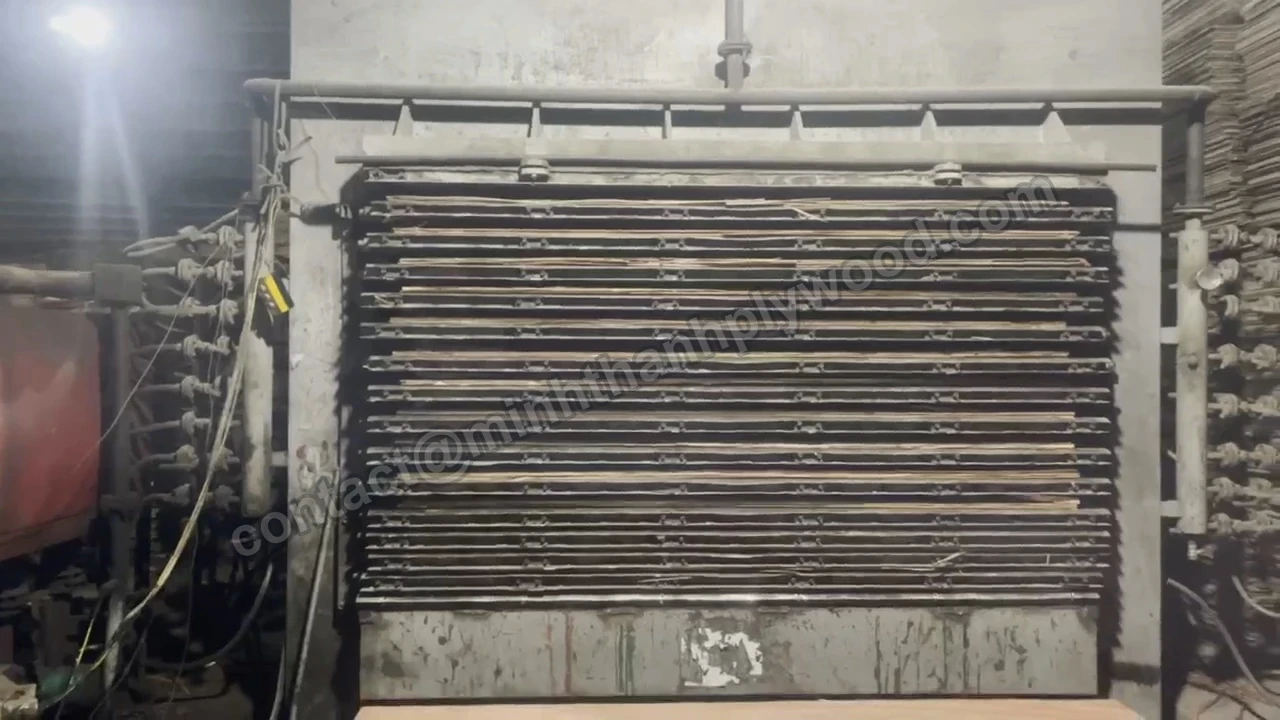
Every opening of the hot press loaded with cores. 07Hot pressing
Pre-pressed panels are loaded into a multi-opening hot press. Heat and 8–12 kg/cm² of pressure cure the glue. Temperature follows the glue: about 110–120 °C for UF and MR glue, 130–145 °C for WBP. Press time follows thickness: about 1 min per mm for UF and MR glue, 1.2–1.5 min per mm for WBP. An 18 mm panel stays in about 18 min with MR glue.
- Press temperature set by glue system
- About 1 min per mm (UF, MR); 1.2–1.5 min per mm (WBP)
- Bond checked on samples after pressing
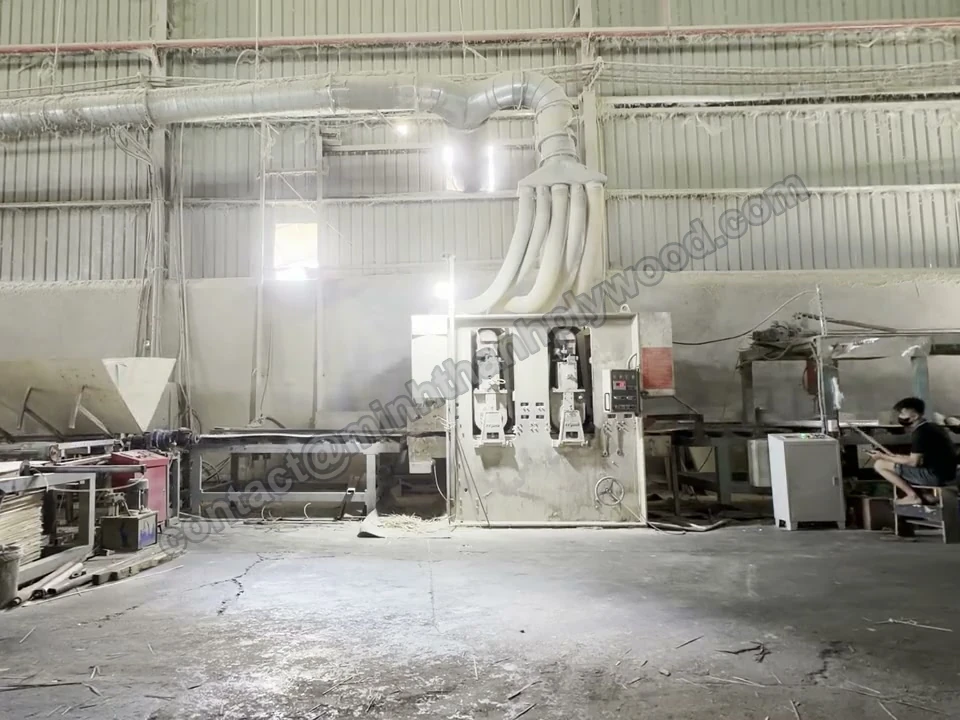
Calibrating sander line for pressed cores. 08Calibrating sanding
After the first press the core is calibrated: a heavy sander takes both sides to an even thickness. This is the step that makes tight tolerances possible, because the faces go onto a core that is already flat and true.
- Core thickness evened before facing
- Both sides calibrated
- High spots and glue lumps removed
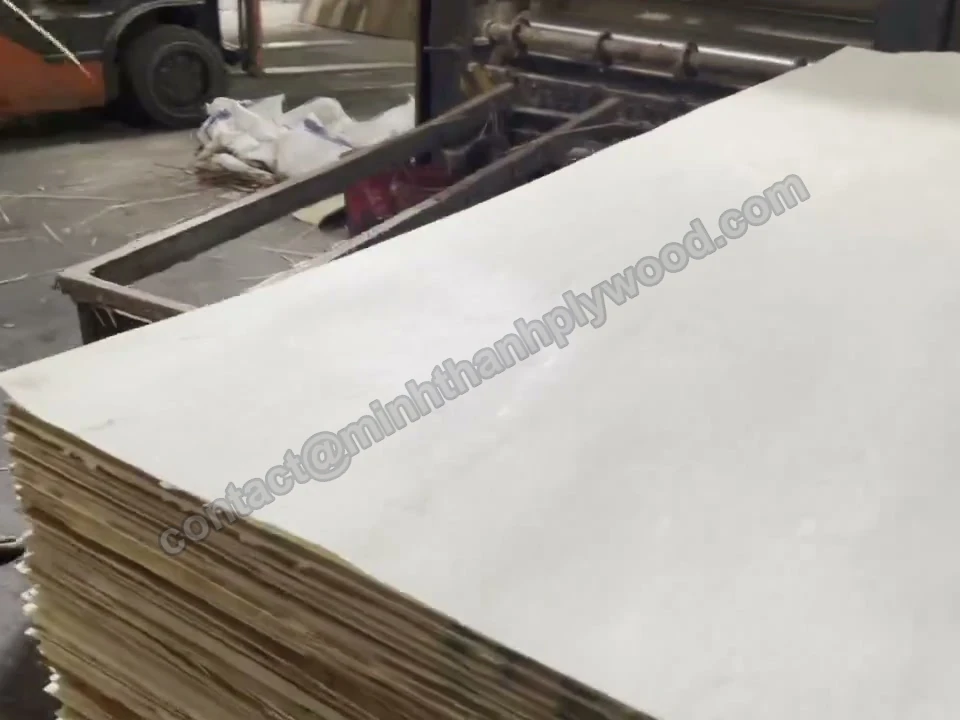
Face veneer laid on calibrated cores before the second press. 09Core repair and face lamination
Open defects in the calibrated core are filled by hand. Then the face and back veneers, 0.2–0.5 mm thick (0.3 mm is common for Europe), are glued on and the panel goes through the press a second time. This two-press method gives a flatter face than pressing core and face in one go.
- Core defects filled before facing
- Face species and grade as your approved sample
- Second press at the temperature of the glue
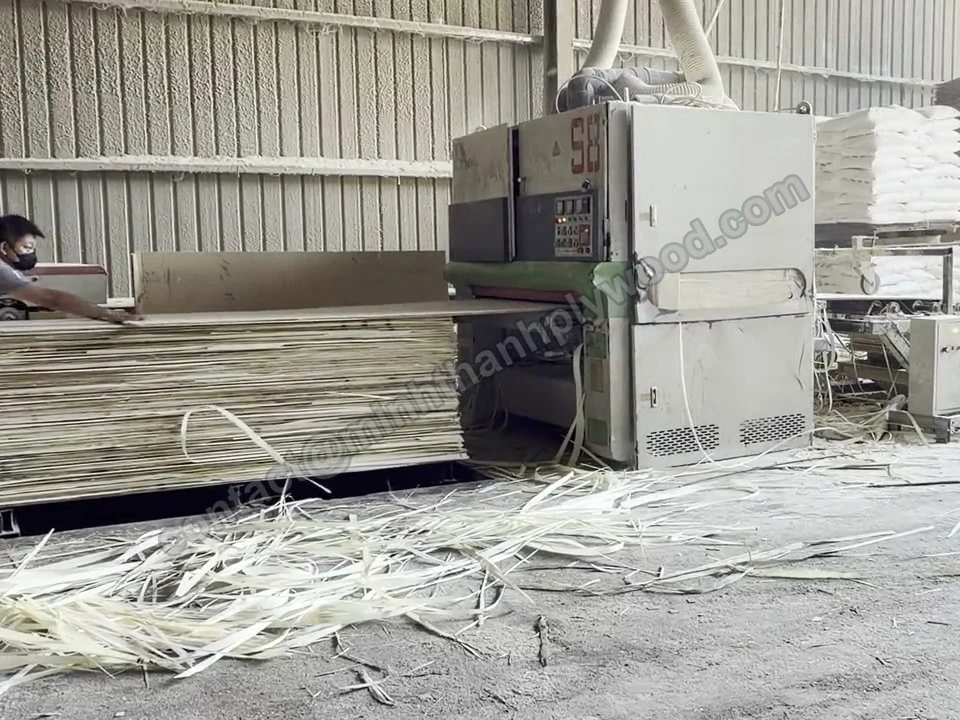
Panels fed into the wide-belt finishing sander. 10Finish sanding and polishing
Faced panels run through wide-belt finishing sanders. Both faces come out smooth and polished, ready for lacquer, paint, foil or the buyer's own UV coating line.
- Both faces sanded and polished
- Faces prepared UV-ready
- Sanding marks and burn-through checked
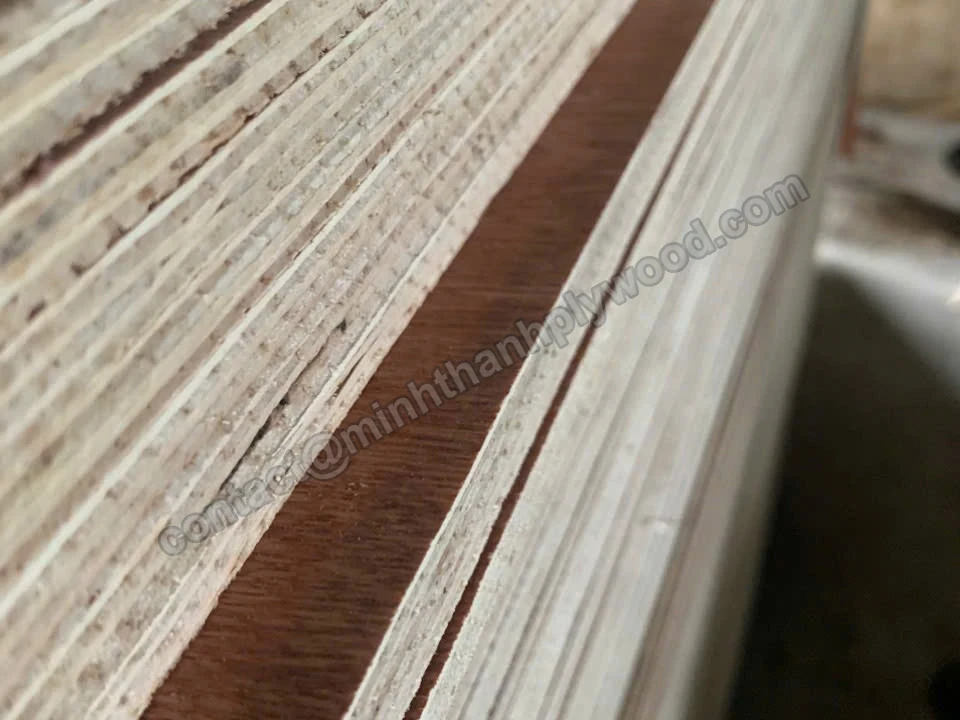
Trimmed edges: every ply shows on the cut. 11Trimming and cut-to-size
Panels are trimmed square to 1220×2440 or 1250×2500 mm, or to custom sizes such as 1220×2500 and 1220×2280 mm. For cut-to-size orders one panel is cut into 4, 6 or 8 pieces, a format we ship regularly to Italy and other European markets.
- Length and width within ±2 mm
- Square, clean edges
- Cut-to-size: 4, 6 or 8 pieces per panel
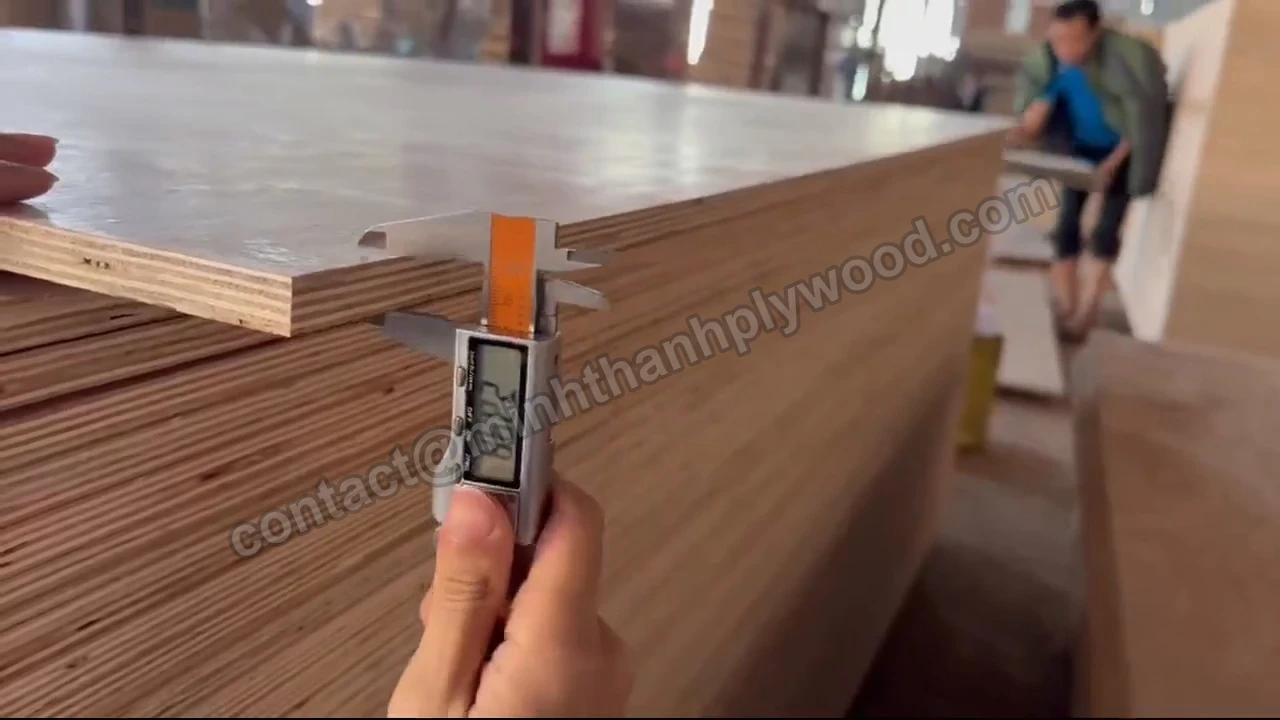
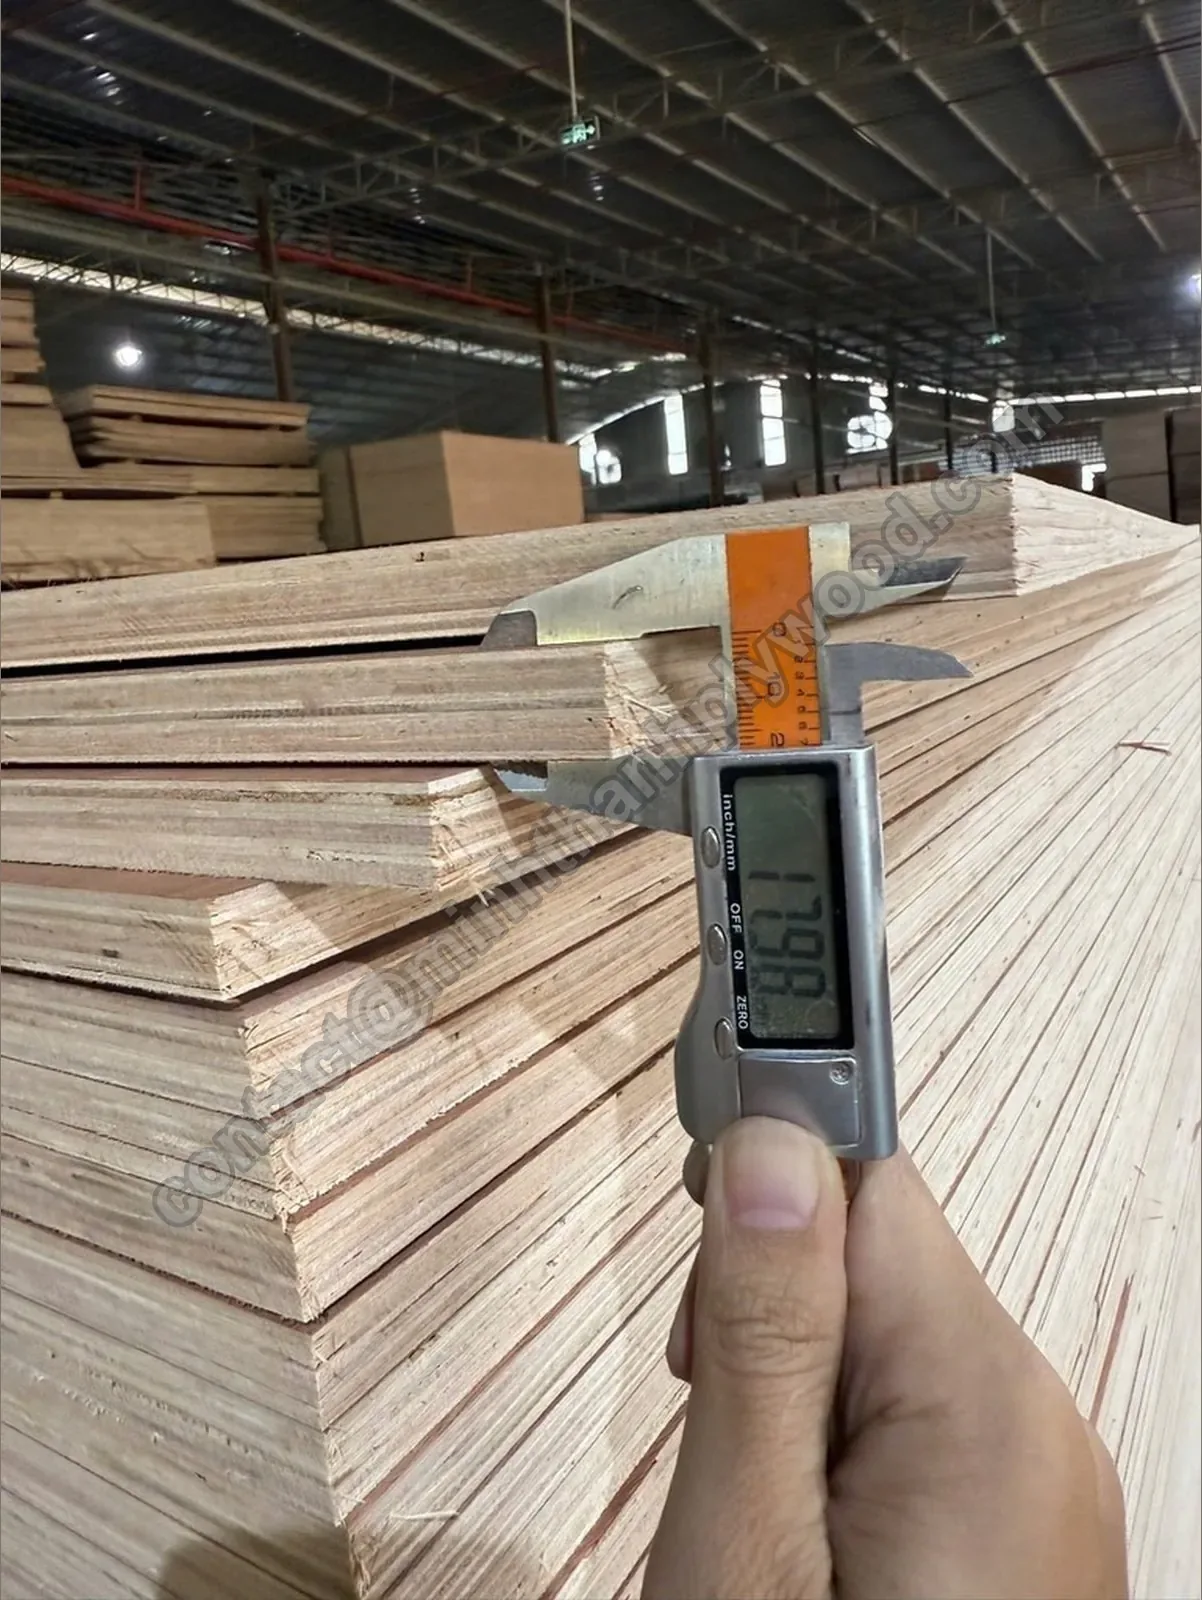
Digital caliper on a panel edge at a finished pack. 12Quality control
Finished panels are checked against the order: thickness with a digital caliper on every pack, faces and edges against the approved sample, glue bond by boil test and sheet count against the packing list. Panels that fail do not go into your order.
- Sanded furniture panels ±0.2–0.3 mm; commercial ±0.5 mm
- Boil test: UF glue at E0 about 6 h, MR about 12 h, WBP the traditional 72 h
- E0 emission tested every 3 months by a third-party lab
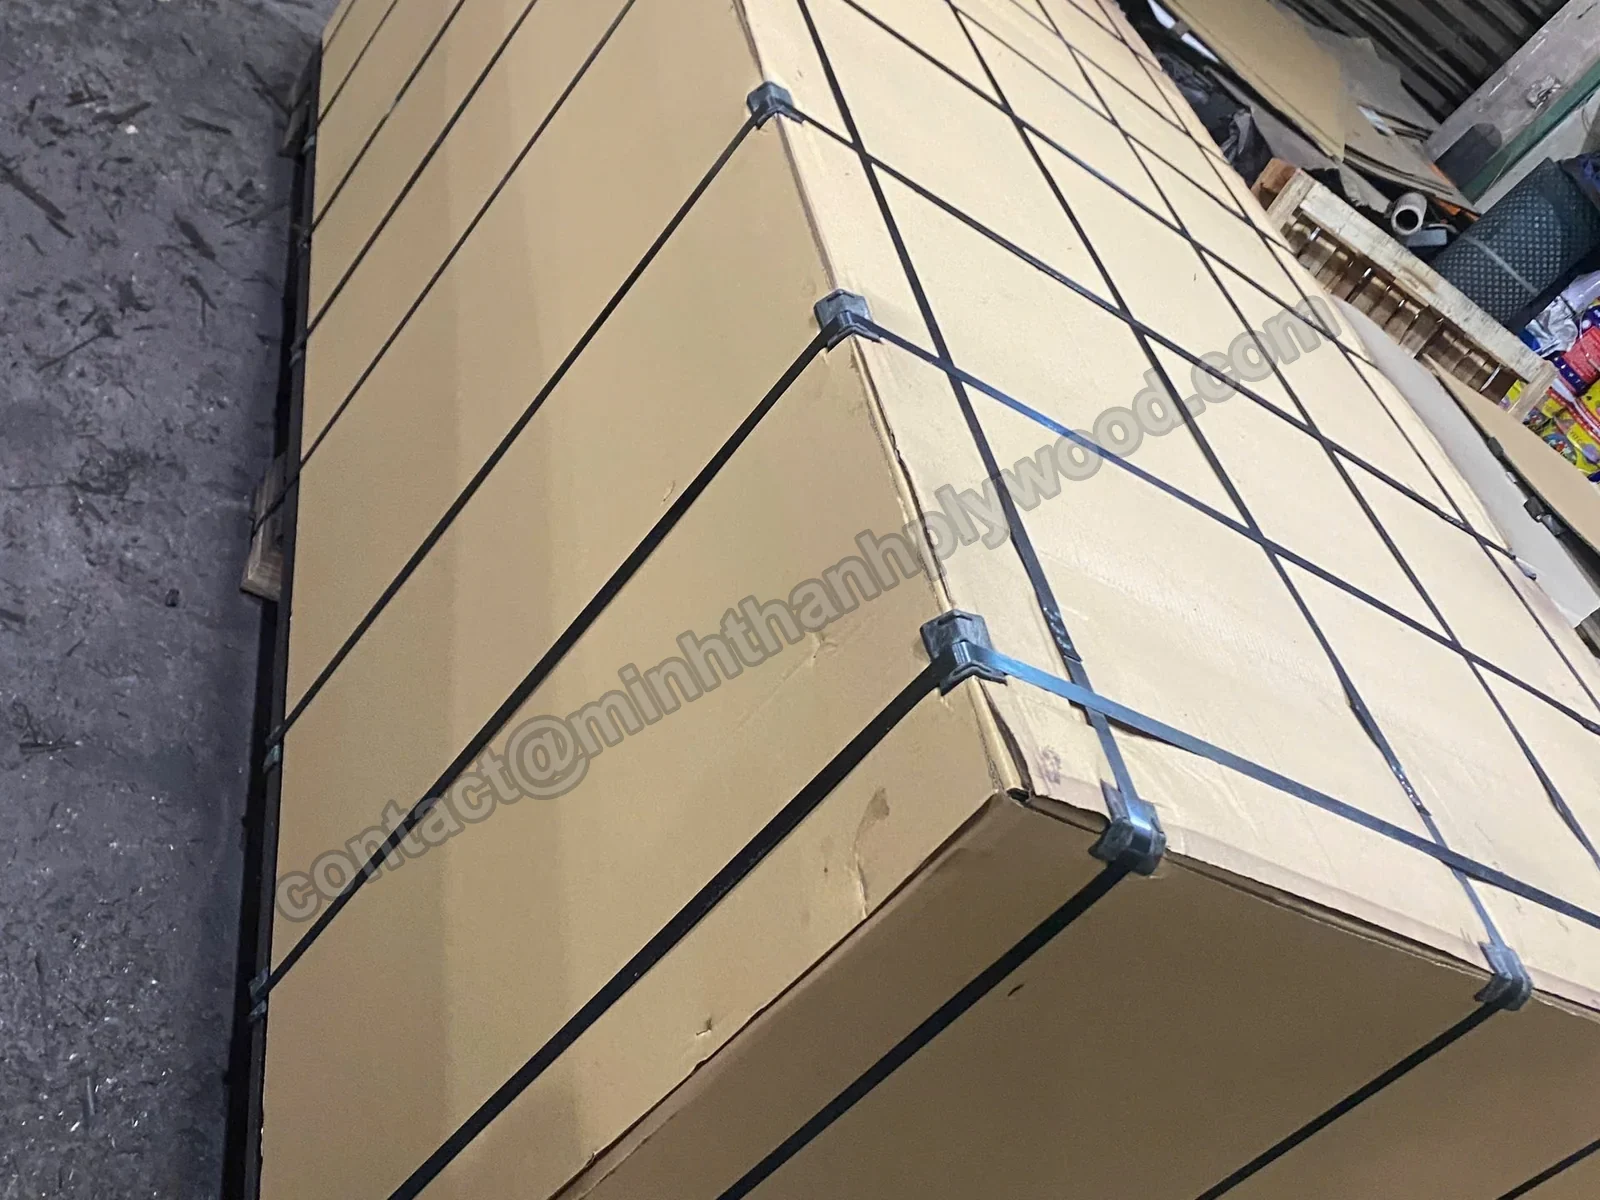
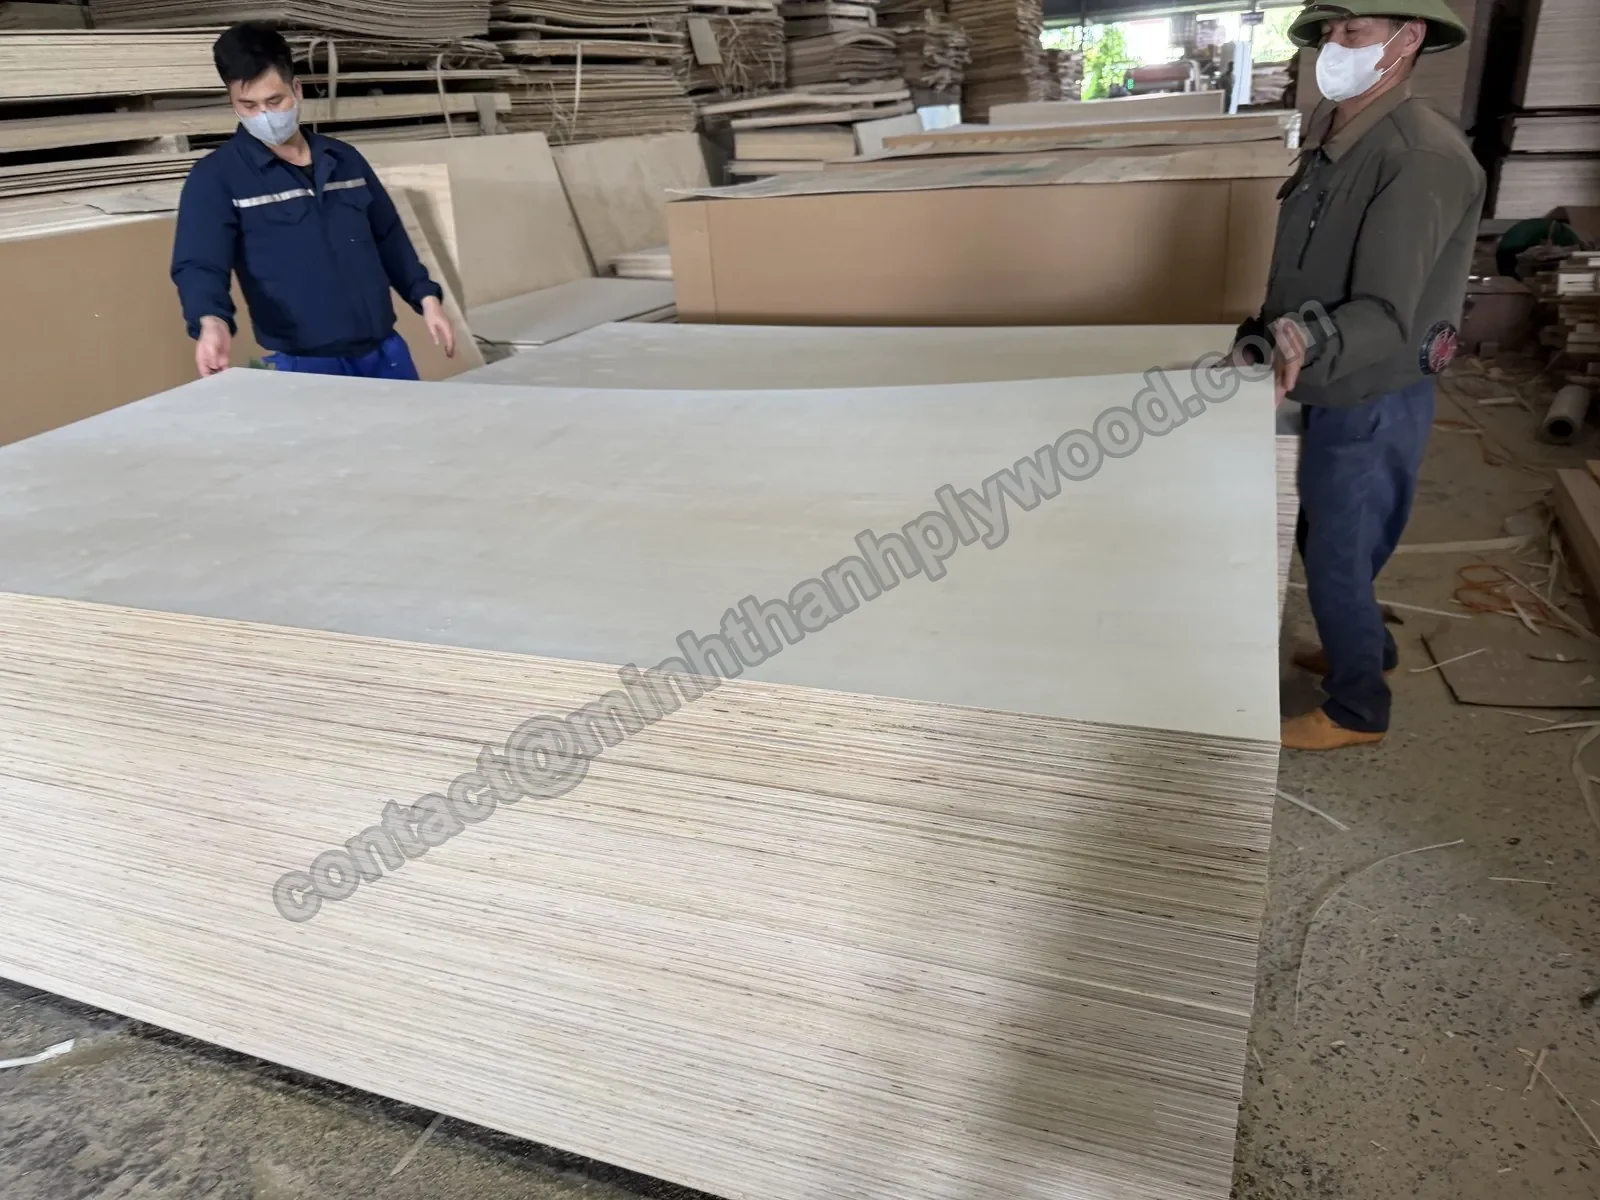
Export pack: cardboard, corners and steel straps. 13Export packing
Approved panels are counted into packs, covered with cardboard, fitted with corner guards and strapped with steel bands on pallets. Pack height is about 1,000 mm, so the sheet count follows the thickness: about 55 sheets of 18 mm or 83 sheets of 12 mm. Your own labels and edge marks are available.
- Sheets per pack checked against the packing list
- Cardboard, corner guards, steel straps, pallet
- Panels packed at 8–12% moisture
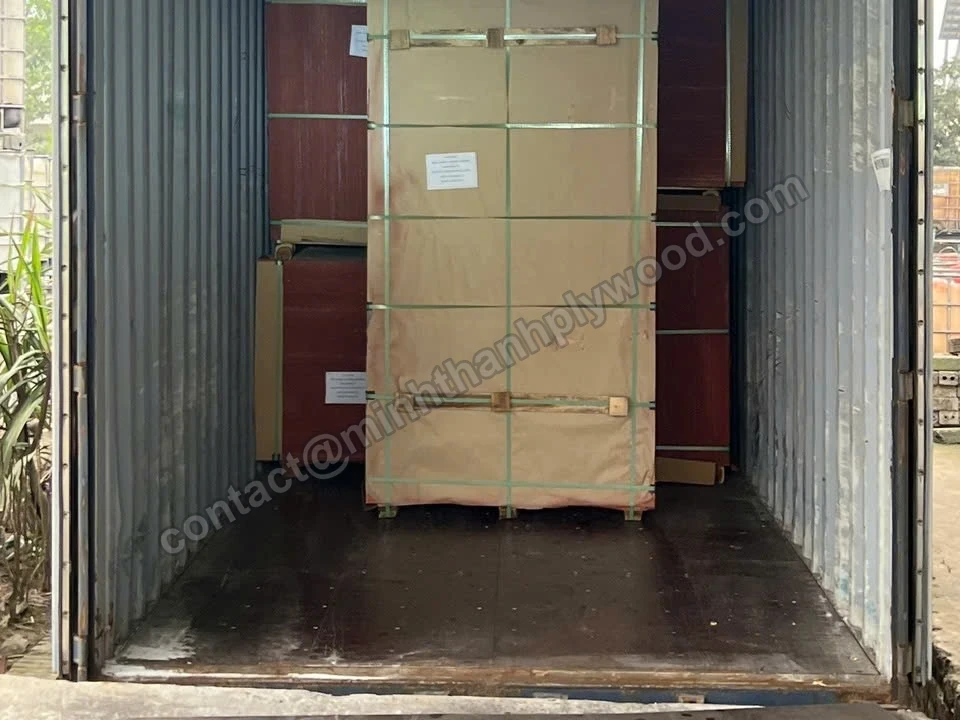
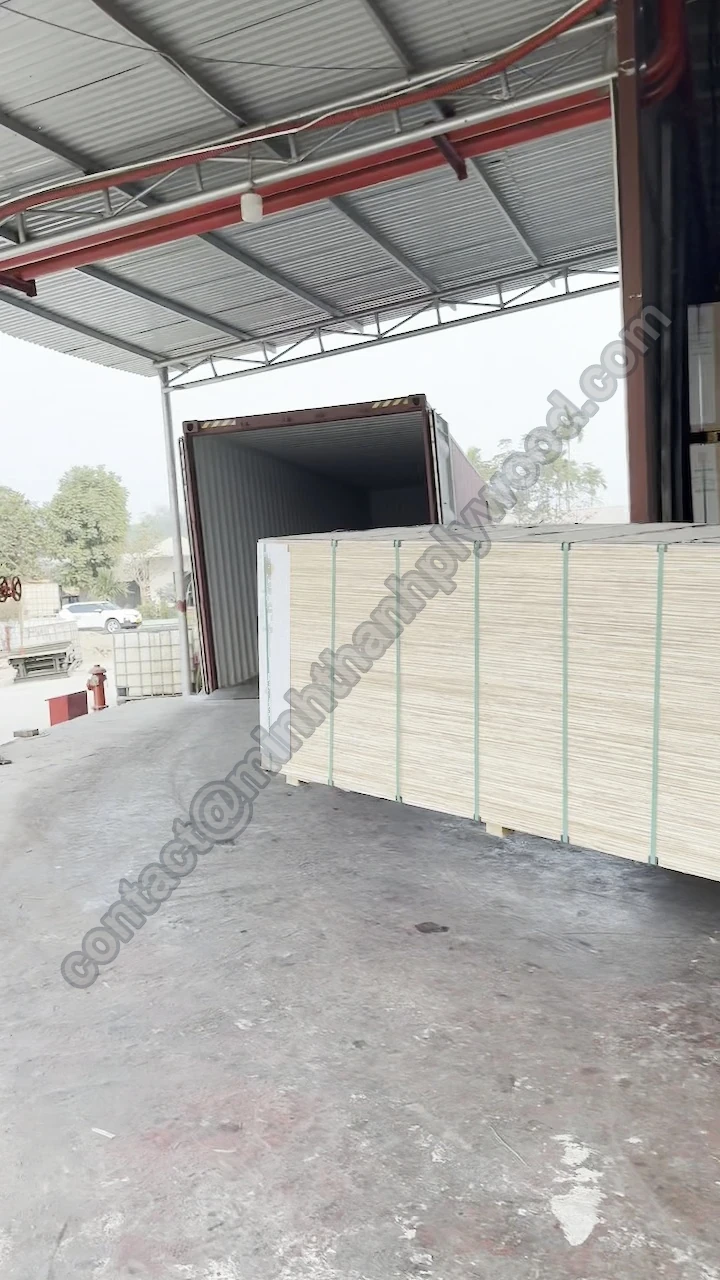
Packs loaded and checked before the doors close. 14Container loading
Packs are loaded by forklift. The container is photographed and filmed before it is sealed. A 40HC takes up to 18 packs with Styrax core (about 53 m³, 26.5 t), 16 with acacia (about 47 m³, 27.3 t) and 15 with eucalyptus (about 43 m³, 27.7 t). Heavier cores reach the payload limit sooner.
- Pack count and labels checked at the door
- Photos and video before sealing
- Load planned by core weight
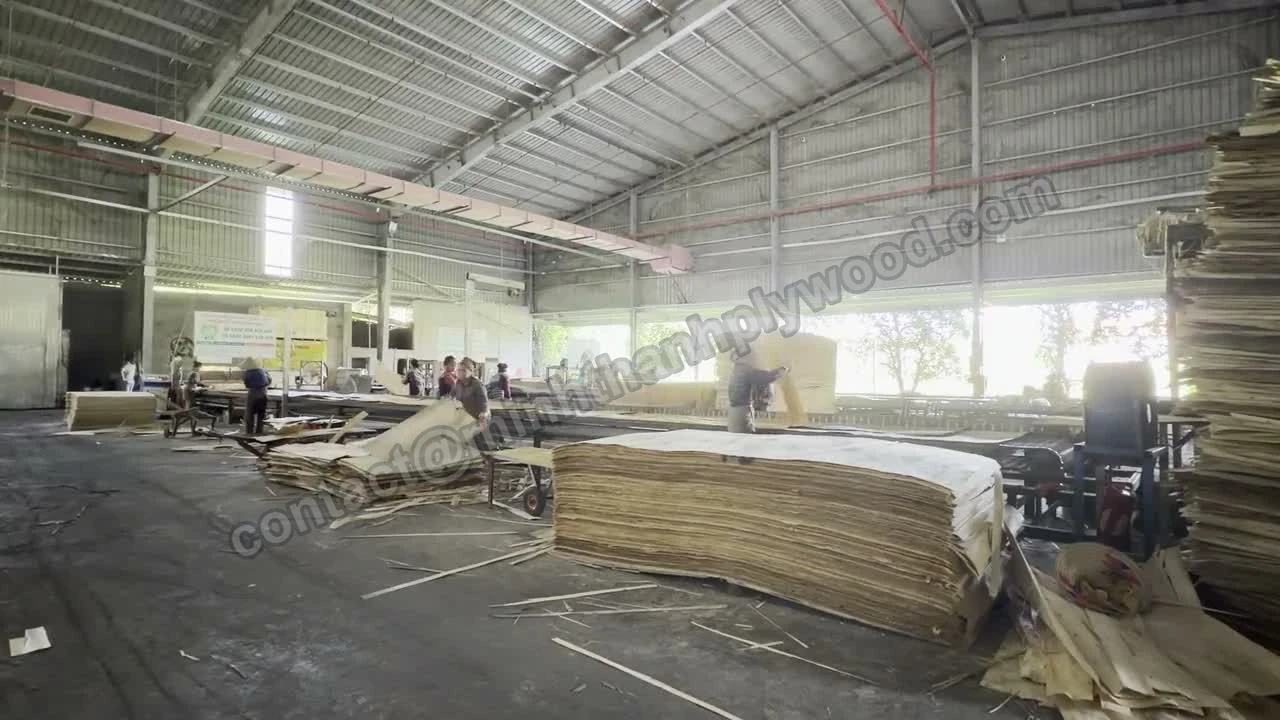
Real production videos
Watch plywood production on the line.
Real clips from our production floor show each stage as it happens, step by step. They play muted when you scroll to them.
Where quality is made
Common plywood defects and the production step that prevents them.
Most plywood defects start at one step of production. Knowing which one tells you what to ask a mill, and what to check on arrival.
| Defect | Usual cause | Prevented at step | How |
|---|---|---|---|
| Core gaps and overlaps | Loose jointing or rushed lay-up | 03 · 05 | Core composer, stitched outer layers, hand lay-up |
| Delamination and blisters | Wet veneer, low glue spread, wrong press temperature | 02 · 04 · 07 | Veneer dried before gluing; glue to order; temperature by glue; boil test |
| Thickness variation | Uneven veneer, press pressure, no calibration | 01 · 08 · 12 | Veneer peeled to size; calibrating sander; caliper on every pack |
| Telegraphing (core showing through the face) | Core gaps under a thin face | 03 · 08 · 09 | Stitched core, calibrated before facing, defects filled |
| Warping | Unbalanced lay-up or uneven moisture | 02 · 05 · 13 | Odd, balanced cross-laid plies; dry veneer; packed at 8–12% moisture |
| Splits, open knots, patches on the face | Face veneer grade | 02 · 09 | Faces graded against your approved sample |
| Sanding marks and burn-through | Worn belts, thin faces | 10 | Finish sanding checked on every face |
| Damaged edges and corners | Handling and transport | 13 · 14 | Cardboard, corner guards, steel straps, pallets; filmed loading |
Plywood production in numbers
What our plywood production delivers.
These are the numbers our line holds, each with the condition it applies to. Your quotation states the values for your own panels.
| Annual capacity | 50,000+ m³ |
|---|---|
| Thickness range | 3–40 mm |
| Sizes | 1220×2440 and 1250×2500 mm; custom such as 1220×2500 and 1220×2280 mm |
| Ply count | Always odd and balanced; 3–5 mm always 5-ply; 18 mm 11–13 plies, most often 11 |
| Veneer thickness | Core 1.4–2.0 mm (1.3 mm in 4 mm panels); face 0.2–0.5 mm, 0.3 mm common for Europe |
| Hot press temperature | UF and MR glue about 110–120 °C; WBP 130–145 °C |
| Cold pre-press | 3–5 kg/cm² for 10–20 min |
| Hot press pressure and time | 8–12 kg/cm²; about 1 min per mm (UF, MR), 1.2–1.5 min per mm (WBP); 18 mm: about 18 min (MR) |
| Thickness tolerance | Furniture, sanded ±0.2–0.3 mm; commercial and film-faced ±0.5; packing ±0.5–1.0 |
| EN 315 sanded allowance (reference) | ±(0.2 + 0.03 × thickness) mm, so 0.74 mm either way at 18 mm. Our sanded furniture panels hold ±0.2–0.3 mm. |
| Length and width | ±2 mm |
| Panel density (reference) | Styrax core about 500, acacia about 580, eucalyptus about 650 (650–750) kg/m³ |
| Sheets per pack | Pack height about 1,000 mm: 18 mm ≈ 55 sheets, 12 mm ≈ 83, 9 mm ≈ 111 |
| 40HC load by core | Styrax 18 packs ≈ 53 m³ ≈ 26.5 t; acacia 16 packs ≈ 47 m³ ≈ 27.3 t; eucalyptus 15 packs ≈ 43 m³ ≈ 27.7 t, at the payload limit |
| Emission class | E0 standard: six ASTM D6007 chamber tests (three by Shanghai Hongjun, three by ICTT Vietnam), April 2025 – June 2026, on 9, 15 and 18 mm panels, 0.014–0.032 ppm against the 0.05 ppm limit; E1 to order |
| Minimum order | 1 × 40HC, mixed loads by agreement |
We weigh real panels before planning every container load, because the core species sets the panel weight.
Sources: EN 315:2000 plywood tolerances (CEN) · California ATCM Phase 2 (arb.ca.gov) · US federal composite wood formaldehyde rule · Quality management standard (iso.org) · ASTM D6007 small-chamber formaldehyde test (ASTM) · Regulation (EU) 2025/40 on packaging (EUR-Lex) · Regulation (EU) 2023/1115, EUDR (EUR-Lex)
Plywood production explained
Why plywood is built this way, and what it means for your order.
Every production step exists to control one of three things: flatness, bond strength or thickness.
Cross-laying is what turns veneer into plywood. Wood moves much more across the grain than along it. Turning each layer 90° locks that movement, which is why plywood stays flat where a solid board would cup. The plies are always odd and balanced around the centre, so both halves pull equally.
Two presses make a better furniture face. In a one-press panel, core and faces are pressed together and any core gap can show through the thin face. We press and calibrate the core first, repair it, then lay the faces and press again. The face goes onto a core that is already flat, so it stays flat after sanding.
Stitched cores stop joints opening. Core veneer is jointed from narrow strips. Stitching the outer 2–4 core layers horizontally and vertically holds the joints closed in the press, which prevents gaps under the face and voids at the edge after cutting.
Glue sets the use. UF glue at E0 emission holds about 6 hours in a boil test and suits furniture and interiors (EN 314 bond class 1, dry use). Melamine-fortified glue holds about 12 hours, usually at E1 emission (class 2, humid use). Phenolic (WBP) glue is pressed hotter, at 130–145 °C, for class 3 exterior use. A boil test checks the bond, not emission; emission has its own lab test.
Dry veneer before glue. Core veneer is dried to 8–12% and every sheet is sorted before lay-up, so wet sheets never reach the glue and the panel does not blister in the press.
Process explains price. Two offers for the same product name are often not the same construction. The difference comes from core grade, joining method, face preparation, adhesive system and tolerance. Compare those five points, not only the product name.
How to tell how a plywood panel was made
Five checks on a sample or on arrival, no lab needed.
- Count the plies at the edge. An odd, balanced number of layers of near-equal thickness shows a cross-laid build; 18 mm should show 11–13 plies.
- Look for core gaps and overlaps. Open joints or doubled veneer at the edge mean loose jointing or lay-up.
- Read the core species. Cream-white is Styrax, pinkish-brown is eucalyptus; mixed colours in one panel mean a mixed core.
- Measure at several points. Use a digital caliper at the corners and long edges; a small spread inside one panel shows calibrated sanding.
- Check the face against light. Hold the panel at a low angle to a light: telegraphing lines or dips show core gaps under the face.
| Item | Furniture & interior | Commercial | Packing | Film-faced |
|---|---|---|---|---|
| Core | A-grade Styrax or eucalyptus | AB-grade core | AB-grade core, laid loose | Acacia or eucalyptus |
| Core joining | Jointed; outer 2–4 layers stitched both ways | Laid or jointed | Laid loose | To film grade |
| Presses | Two presses: core, then faces | One or two presses | One press | Core press, then film press |
| Sanding | Calibrated, then sanded and polished; UV-ready | Light sanding or unsanded | Unsanded | Core calibrated; film face |
| Glue and emission | UF glue, E0 standard; MR or WBP glue and E1 to order | To order | To order, often E2 | Melamine or phenolic (WBP) |
| Thickness tolerance | ±0.2–0.3 mm | ±0.5 mm | ±0.5–1.0 mm | ±0.5 mm |
| Typical uses | Cabinets, furniture, CNC parts, shopfitting | General building and joinery | Crates, pallets, cases | Concrete formwork: about 12–15 pours with melamine, up to about 25 with phenolic |
The last step
Every shipment photographed and filmed.
Before the container is sealed you receive photos and video of your order by email or WhatsApp, the same record we use to release the shipment, and the shipping documents follow with the B/L.
- Caliper readings on panels from every pack
- Faces, backs and edges of sample panels
- Packs with labels, corner guards and steel straps
- The container during loading and fully loaded
- Commercial invoice, packing list, B/L, certificate of origin (EUR.1 for the EU on request)
- Phytosanitary and fumigation papers where the market asks; insurance with CIF
- The EUDR compliance dossier (origin records and geolocation files)
- Your own inspector or a third-party agency is welcome before loading
Want to see your panels earlier? Ask for photos at lay-up or after the first press.
Production lead time
From specification to sealed container.
Production starts on the deposit; quantity and face veneer decide how long it takes. This is how an order moves from specification to a sealed container.
Specification and sample
You send end use, core, glue, face, thickness, size and quantity. The quotation states construction and tolerance; free samples.
Deposit and materials
After the 30% deposit we book core veneer and face veneer for your order. Premium thin veneer for 4 mm panels can take longer.
Core making and first press
Drying, sorting, jointing, stitching, glue, lay-up, cold and hot pressing, then calibration.
Facing and finishing
Core repair, face lamination and second press, finish sanding, trimming or cut-to-size.
Inspection and packing
Quality control on every pack, your inspector if booked, export packing and draft documents.
Loading and balance
Loading filmed and sent to you, FOB Hai Phong, CFR or CIF; the 70% balance is due against the scanned B/L.
Mixed loads of 1–2 products per container are normal; 3–6 by agreement.
Capacity
50,000+ m³ a year: about 940 containers.
At about 53 m³ per 40HC, 50,000+ m³ a year is roughly 940 containers, or 75–80 a month. One container or several a month fit our normal schedule. Furniture and interior panels lead; commercial, packing and film-faced lines run through the same steps and checks.
About the factoryBefore you order
Six lines that set the whole production run.
These six lines are enough for an exact quotation.
- 01
End use
Furniture, cabinets, packing, formwork or flooring; indoor or outdoor.
- 02
Core and joining
Styrax or eucalyptus core; stitched or not, and how many layers.
- 03
Glue and emission
Glue type (UF, MR or WBP), emission class E0 or E1 for your market, and any boil-test requirement.
- 04
Faces
Face and back species, veneer thickness, grade by approved sample, sanded or polished, UV-ready.
- 05
Panel
Thickness, size, tolerance by line, cut-to-size if needed.
- 06
Packing and quantity
Pack type, labels, quantity, port, documents and test reports.
Questions buyers ask
Plywood manufacturing process FAQ.
Short answers to the questions buyers ask most about manufacturing.
What is plywood made of?
Wood veneer and glue. Our cores are Styrax or eucalyptus from plantations around Ha Hoa; commercial and film-faced lines also use acacia. Faces are EV, poplar, birch, okoume, pine and others. Glue is UF as standard, with MR or WBP to order. Emission is E0 as standard, E1 to order.
How long does a plywood order take to produce?
An export order takes 15–45 days after the deposit; quantity and face veneer set where it falls in that range. Orders of 4 mm panels take longer because premium thin veneer is scarce, and we do not lower the standard to go faster.
How long is plywood pressed in the hot press?
About 1 min per mm of thickness with UF or MR glue, at 110–120 °C and 8–12 kg/cm²; phenolic WBP glue takes 1.2–1.5 min per mm at 130–145 °C. An 18 mm panel stays in the press about 18 min with MR glue. Furniture faces go through a second, shorter press after the core is calibrated.
Why does plywood always have an odd number of plies?
An odd number puts one layer at the centre with the same build on both sides, so the panel pulls equally and stays flat. Thin 3–5 mm panels are always 5-ply; 18 mm panels are 11–13 plies, most often 11.
What is the boil test for plywood?
A boil test soaks plywood samples in boiling water for a set time, then checks the glue lines for delamination. Our UF panels at E0 hold about 6 hours and melamine-fortified panels about 12 hours. It tests bond strength, not formaldehyde emission.
Are glue type and emission class the same thing?
No. The glue type (UF, melamine-fortified MR or phenolic WBP) sets bond strength and water resistance. The emission class (E0 or E1) sets how much formaldehyde the panel releases. A specification names both, for example "MR glue, E1" or "UF glue, E0".
What temperature is plywood pressed at?
Pressing temperature follows the glue. UF and MR glue are pressed at about 110–120 °C and phenolic (WBP) glue at 130–145 °C. Pressing time follows the thickness of the panel, and every press load is checked for bond afterwards.
What is the difference between one-press and two-press plywood?
In one-press plywood the core and faces are pressed together. In two-press plywood the core is pressed, calibrated and repaired first, then the faces are glued on and pressed again. Two presses give a flatter face with less telegraphing, which is why we use them for furniture panels.
How dry is the veneer before gluing?
Veneer is dried until its moisture suits the glue, 8–12%, and wet sheets are sorted out before lay-up. Finished panels are packed at 8–12% moisture so they stay flat in transit.
Is Vietnamese plywood made with poplar or birch cores?
No. Vietnamese plywood cores are Styrax, eucalyptus, acacia or mixed. Birch-faced and poplar-faced plywood use face veneer on a Vietnamese core, so the product is named after the face.
What thickness tolerance does the process hold?
Sanded furniture and interior panels are held to ±0.2–0.3 mm. Commercial and film-faced plywood is ±0.5 mm and packing plywood ±0.5–1.0 mm. Length and width are ±2 mm.
Which glue should I choose?
UF glue at E0 emission for furniture and interiors; it holds about 6 hours in a boil test. Melamine-fortified (MR) glue for damp or outdoor use holds about 12 hours, usually at E1 emission. Phenolic (WBP) for formwork and exterior panels. Tell us the end use and we propose the glue.
How do I know a supplier is a real manufacturer?
Ask for photos or video of your own order at lay-up, pressing and loading, and check the mill numbers on the issuers' registers. We send a photo and video record of every shipment, and your inspector is welcome at the factory.
Can I send an inspector during production?
Yes. Your own inspector or an agency such as SGS, Intertek or Bureau Veritas is welcome during production or before loading. Give us the date with the order and we plan around it.
Get a quotation
Send your specification; we plan the production run.
Tell us the end use, core, glue, face, thickness, size and quantity. We reply with the construction, tolerance and lead time for your panels. Lisa replies within hours by email or WhatsApp. Free samples.
contact@minhthanhplywood.com